Oct 27, 2026Quality Assurance
Design Tips for CNC Turned Parts
Small drawing decisions decide machining cost long before a quote arrives. Six design habits make a turned part easier to manufacture without asking for less from the part.
Most of a turned part's machining cost is decided at the drawing stage - before any supplier sees it. A tight tolerance applied well beyond the two features that need it, a groove in a hard-to-reach place, a finish callout on a face nobody sees: none of these make the part better, but each makes it harder to make. Six design habits keep a drawing manufacturable: tolerance economy, standardized features, reachable geometry, finishes only where they matter, explicit threads, and datums before dimensions.
Tighten Tolerances Only Where They Earn Their Keep
Specifying general tolerances to the drawing, with tighter control reserved for selected features, is how turned parts are economically detailed. On Yongxin's turning route, turning tolerances to +/-0.005 mm are held, and selected features can reach +/-0.002 mm where function demands it - figures to check against your own drawing rather than apply everywhere. A drawing full of tight tolerances does not read as careful design; it reads as a drawing whose critical features are hard to find.
Standardize Features Across the Part
As general design-for-manufacturing practice: where several holes, grooves or threads serve the same function, giving them the same specification lets one tool do all of them. Every distinct tool size adds a tool change, and tool changes on a turning center add cycle time and another setup-related variable. Fewer distinct features also simplify inspection - and simplify the drawing review, because there are fewer special characteristics to negotiate.
Keep Features Reachable by the Process
Turning and turn-mill machining reach certain geometries naturally and strain at others. Very deep narrow grooves, internal undercuts behind shoulders, and cross features positioned where no standard tool can approach them all force special tooling or secondary operations. Before finalizing geometry, it pays to ask whether a feature could be relocated, opened up, or replaced with a form that a standard tool reaches - the function usually survives, and the route stays on one machine.
Call Out Finishes Where They Matter
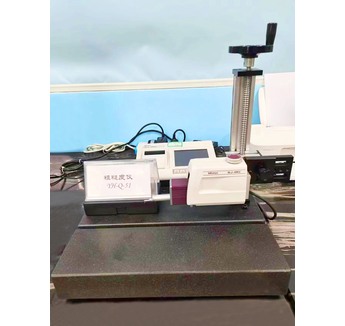
Surface finish and coating callouts work the same way as tolerances. Where sealing or fatigue matters, call the finish out explicitly - on turned surfaces, surface roughness down to Ra 0.4 um is achievable. Finishing support covers the full range: passivation and black oxide, zinc, nickel and chrome plating, anodizing and hard anodizing, PVD, polishing and sandblasting, plus laser marking and cleaning. Specifying a heavy finish on every face forces the whole part through the most expensive route; specifying it on the functional surfaces keeps both the part and the plating bath happy.
Specify Threads Explicitly
Threads are a classic source of first-sample surprises: name the standard and class rather than leaving them to assumption, because thread systems differ by region and an unspecified callout invites a mismatch discovered at assembly. The habit costs one line on the drawing and removes a correction loop.
Define Datums Before Detailing Dimensions
Define which surfaces the critical dimensions measure from. Feature-to-feature relationships - concentricity between a bore and its mating shaft, position of a cross hole against a bore - are only as good as the datums they reference, and inspectors can only check what the drawing defines. Datums first, then dimensions, is the order that survives review.
Boundaries and Next Step
These habits shape a drawing; they do not replace the review. Final feasibility depends on part geometry, material condition, process route and inspection method, and it is confirmed per drawing - together with price and lead time at feasibility stage. If you have a drawing heading for quotation, send it with material, annual volume and quality requirements; practical manufacturing feedback on the design is part of the review.