Oct 15, 2026Engineering Options
The Hidden Cost of Secondary Operations on Turned Parts
Every extra setup on a turned part adds tolerance drift, handling and queue time. What one-setup turn-mill machining changes - and what to ask before you order.
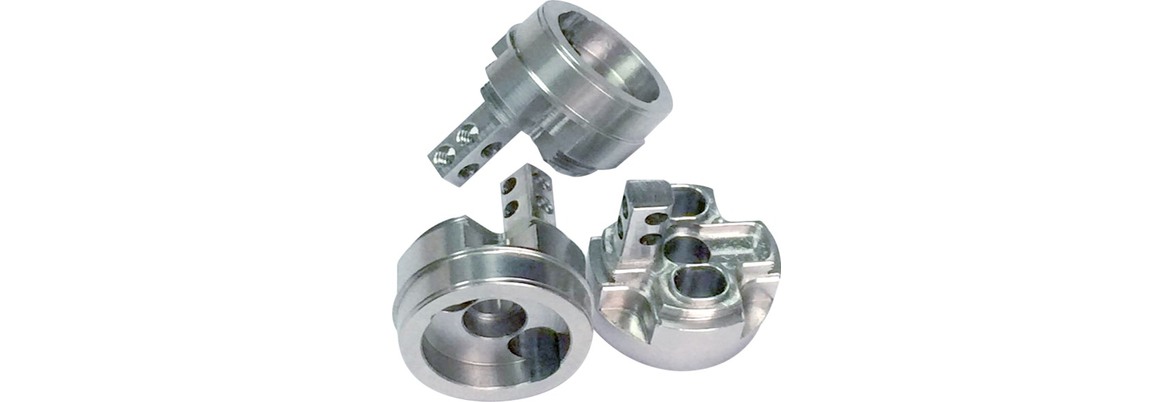
Every time a turned part leaves its machine for a second operation, three costs start accumulating: tolerance drift from re-clamping, handling labor, and queue time between departments. On parts with flats, cross holes or slots these costs grow with every added feature - and they surface late, as assembly problems and missed launch dates.
What Secondary Operations Actually Cost
The common pattern: parts are turned on a CNC lathe, then moved to a milling machine for flats, cross holes or slots. Every re-clamp erodes the coaxiality and position accuracy the turning operation had already achieved. Each extra process also adds labor, another quality risk, and queueing time of about a week - which is how time-to-market gets dragged down by operations that did not appear on the original quotation.
What One-Setup Turn-Mill Changes
One-setup machining removes that chain. On turn-mill centers and Swiss-type lathes, turning, milling, drilling and back-working complete in a single clamping: coaxiality can hold within 0.005 mm because the part is not re-fixed between operations, and the queue between operations is designed out. On programs converted from multi-operation routes, Yongxin commits to turnaround cost and lead time reductions of 20% or more.
When One Setup Matters Most
The benefit grows with feature count: cross holes, slots, flats and multi-feature geometries on automotive, hydraulic and connector parts are where secondary operations pile up fastest. For simple, tolerance-free parts a second operation may be harmless - which is exactly why the drawing review should decide the process route, not habit.
What to Ask Your Supplier
How many setups does this part need, and where is coaxiality verified? Which features are completed in one clamping? What queue time sits between operations? Suppliers who machine the part in one setup can answer all three from process sheets rather than estimates.
Boundaries and Next Step
Final feasibility is confirmed per drawing: geometry, material condition, process route and inspection method decide what can be held. Price and lead time are quoted at the feasibility stage, and an NDA is available before drawings are shared.